Hardware & small welded parts
Hinge and pin joint
Review part location, joint access, repeatability and required joint inspection.
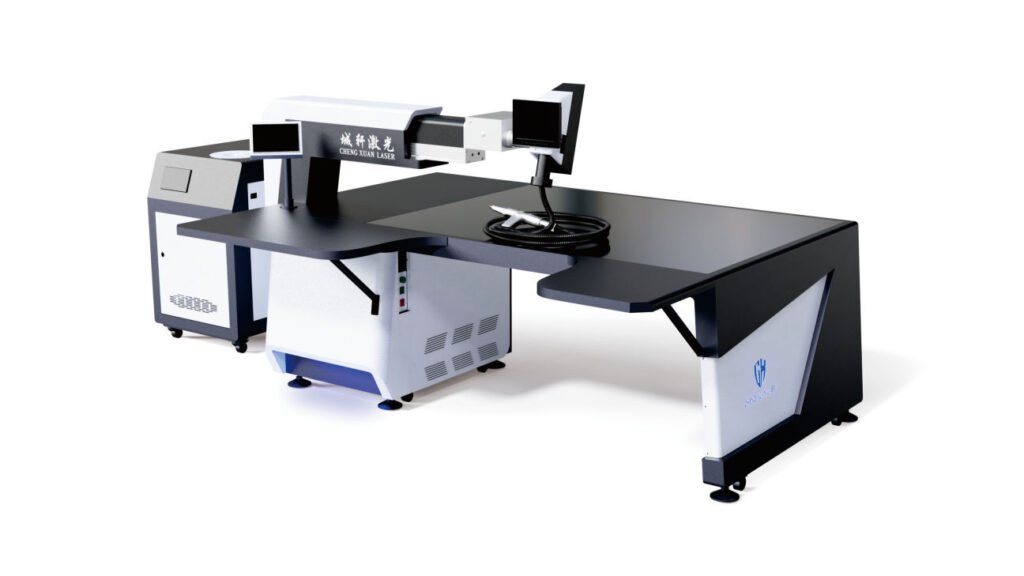
Manufacturer series reference image. Final appearance and accessories are confirmed for the selected configuration.
See the machine. Discuss the process.Request current photos and a real demonstration↗CX-2217 catalogue family
A YAG pulse welding table for handheld and benchtop operation. Discuss the part, joint and preferred work layout.
Review this configuration alongside the equipment and utilities your process needs.
Supplied Chengxuan Laser English Catalogue 2026, PDF page 43
Family-level values are references. Confirm the selected system and application before an order.
| Laser power options | 300 / 500 W |
|---|---|
| Oscillation frequency | 0–60 Hz |
| Wavelength | 1064 nm |
| Focusing distance | 200 mm |
| Operation | Manual handheld / benchtop |
| Aiming | Red light / CCD |
| Reference dimensions | 2300 × 1200 × 1300 mm |
| Reference machine weight | 300 kg |
Process capability, duty cycle, safety measures, electrical requirements, included accessories and delivery conditions are confirmed for your application. Request the current model-specific documentation with your enquiry.
Handheld, pulse and production welding configurations, reviewed around your material, joint access and daily workload.
Laser Welding Solutions ↗Bring metal faces, formed returns and QCW or another validated welding process into one sign-making workflow. Add acrylic cutting, finishing and lighting assembly where the letter design calls for them.
| Supporting equipment | Role in the package | What to confirm |
|---|---|---|
| Channel Letter Bending Machine | Core workflow | Recommended for in-house return forming. Review coil compatibility, slotting/notching and bending functions; existing equipment or bought-in returns are alternatives. |
| Welding Tables and Application Fixtures | Required provision | Provide suitable letter workholding and joint access for the selected weld process. |
| Application-Matched Fume and Dust Extraction | Required provision | Review separate capture needs for welding, cutting and finishing; one extractor is not assumed suitable for every process. |
| Laser Process Enclosure and Interlocks | Required provision | Confirm laser work-area protection for the QCW or other selected welding equipment. |
| Industrial Laser Water Chiller | Process dependent | Check the selected QCW/welding cooling requirement and whether a chiller is included. |
| Assist and Shielding Gas Supply System | Process dependent | Confirm shielding and other utility-gas requirements for the actual process. |
| Laser Cutting Air Compressor System | Process dependent | Check bender actuation and cutter demand against the available air supply. |
| Compressed Air Dryer | Process dependent | Add the required drying if the existing supply does not meet the selected machines specification. |
AI-restored from supplied catalogue photographs for clearer browsing. Compare originals; confirm fine details on your sample.
Review part location, joint access, repeatability and required joint inspection.
Review seam continuity, heat effects, surface finish and the agreed inspection method.
Review corner geometry, fixture access, appearance and assembly dimensions.
Review part location, joint access, repeatability and required joint inspection.
Review part location, joint access, repeatability and required joint inspection.
Review part location, joint access, repeatability and required joint inspection.
Request a written quotation for the selected configuration. Include the material, part drawing or dimensions, workload, available utilities and delivery city. The quotation confirms the equipment, accessories, freight and service scope; a catalogue reference is not a confirmed order specification.
Request a configuration quotationDiscuss these related items as part of the complete production route:
Review compatibility, existing equipment and what is already integrated before adding separate equipment. Supporting items are application-matched; the quotation confirms the supplier and included scope.
Technical reference: CX-2217-PULSE · Catalogue PDF, page 43
A YAG pulse welding table for handheld and benchtop operation. Discuss the part, joint and preferred work layout. Its catalogue family is CX-2217. The listed power or configuration is 300 / 500W and cooling is Water-cooled.
For this laser welding configuration, share the material grade, thickness, joint geometry, seam access and daily workload. Include available electrical supply, utilities and the destination country, delivery city or postcode.
The technical table uses family-level references from Supplied Chengxuan Laser English Catalogue 2026, PDF page 43. Confirm the exact model, selected output, electrical supply, accessories and process capability in a written quotation.
Yes. Use the product enquiry form or WhatsApp +86 189 7513 5599 to request a quotation and ask about a current demonstration or a material sample test. Availability and test conditions require confirmation. An enquiry does not create an order or collect payment.
Share the material, required process and destination. Add production details and supporting equipment where useful.
Your enquiry is linked to this machine. Share your application so we can confirm the configuration.